 English
 Français
 Deutsch
 Español
 Italiano
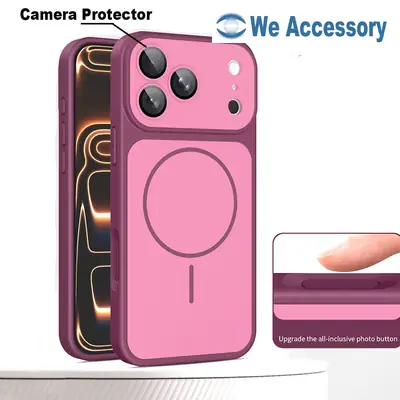
iPhone 18 Pro Max Skin-feeling magsafe case Matte case with build-in camera protection
Recommend Products
-
-
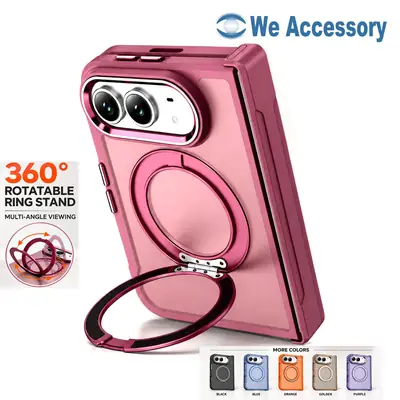 iPhone Duo 360° rotating ring holder case N52 2300 Gauss strong magentic stand case
-
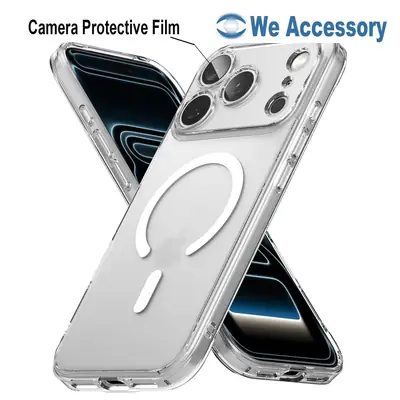 iPhone 18 Pro Clear Magsafe Case build-in camera protector transparent magnetic case
-
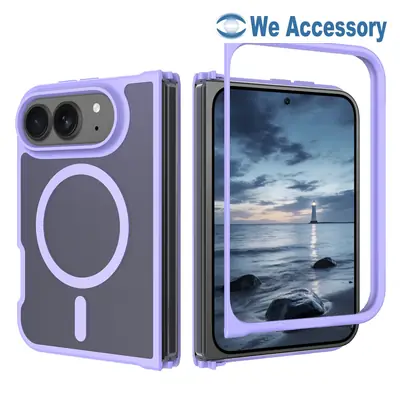 iPhone Duo Matte Magsafe Case Skin-Feeling N52 Strong Magnetic 2in1 Foldable Case
-
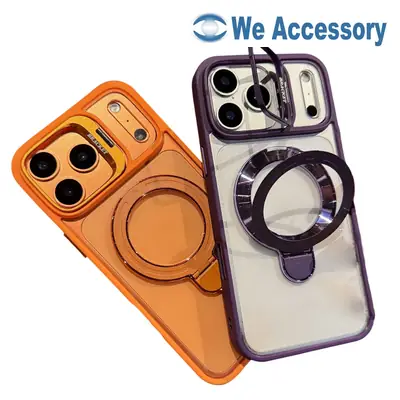 iPhone 18 accessories iPhone 18 Pro 3in1 magnetic holder case camera holder ring holder case
-
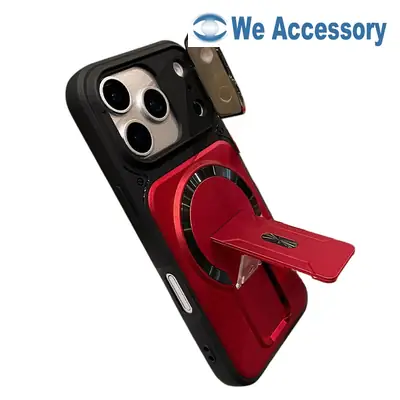 iPhone 18 Pro magsafe holder case glass camera protection and foldable holder case
-
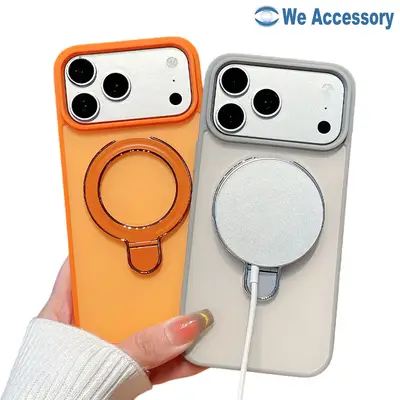 New trend iPhone 18 Pro matte skin-feeling magsafe case ring holder phone holder case
-
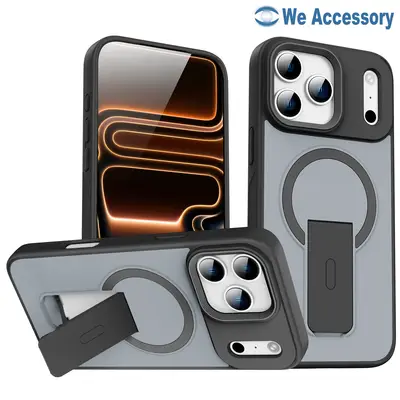 Hot phone accessories iPhone 18 Pro magnetic stand phone case foldable phone holder case
-
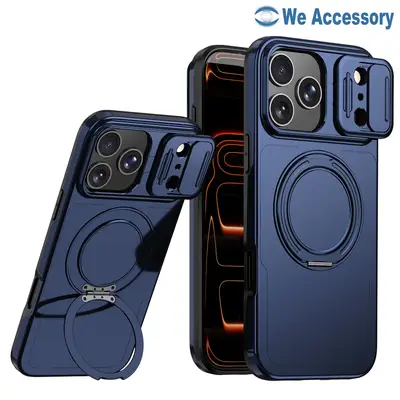 New iPhone 18 Accessories iPhone 18 Pro Ring Holder Case Camera protection Magsafe Case
-
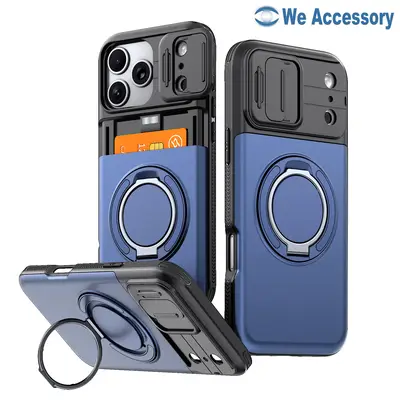 iPhone 18 Pro Max Card Holder Case Magsafe Holder Case Slide Window Camera Protection
-
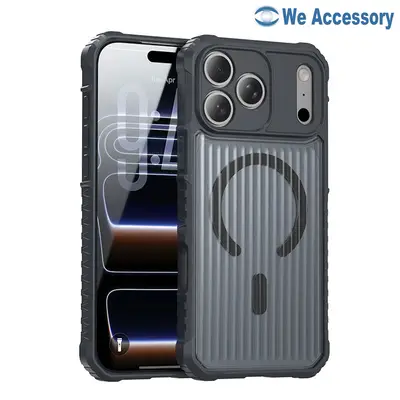 New design iPhone 18 Pro TPU+PC Hybrid Suitcase-Style MagSafe Shatterproof Case
-
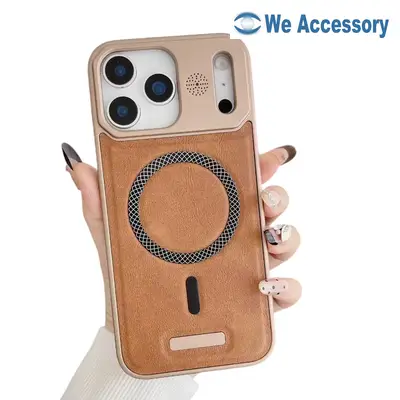 Business demeanor iPhone 18 Pro magsafe leather case 2in1 iphone cover luxury iphone case
-
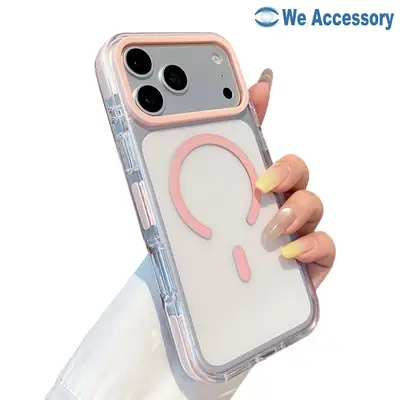 New iPhone Accessories iPhone 18 Pro Clear Magsafe Case double color 2in1 shatterproof case
-
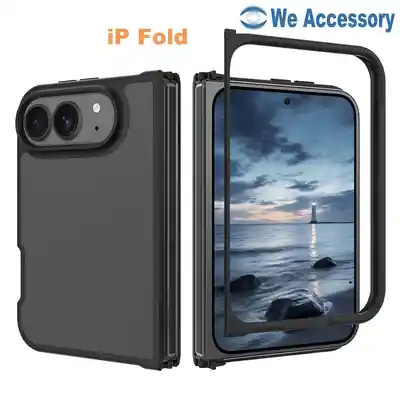 iPhone Case Distributor Newest iPhone Fold Case TPU+PC 2in1 Full Protective iPhone Case
-
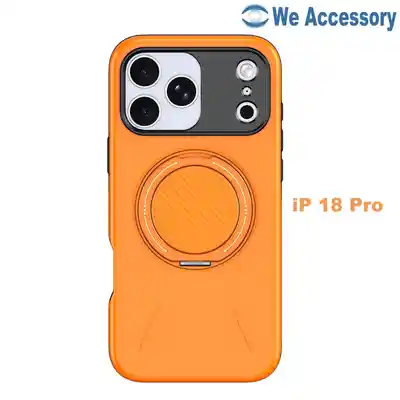 Phone Accessories Company New iPhone 18 Pro Case Magsafe Case with Phone Holder
-
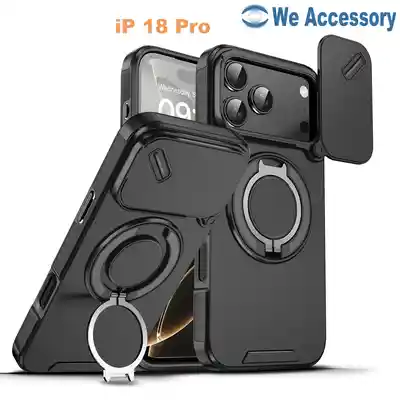 Phone Case Manufacturer New iPhone 18 Pro Max Armor Case Camera Protection and Holer
-
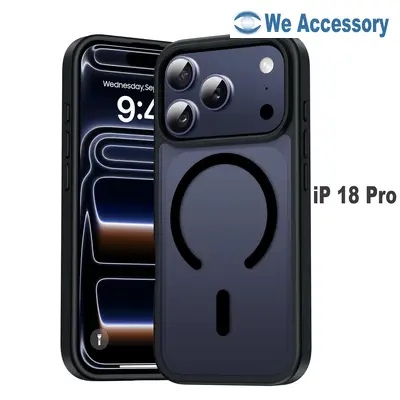 iPhone 18 Accessories Supplier Newest iPhone 18 Pro Case Wholesale Matte magsafe case
-
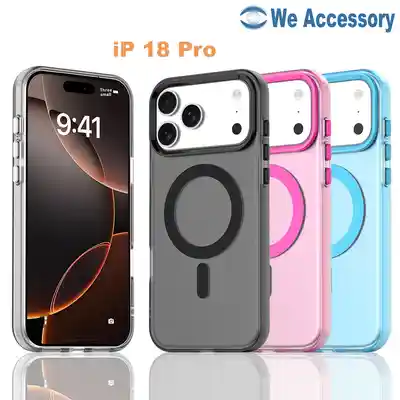 iPhone 18 Pro Case Wholesale Colorful Transparent Magsafe Case New iPhone 18 Pro Case
-
 Wholesale iPhone 17 Jelly 2 in 1 Magsafe Case colorful silicone iphone case
-
 Apple iPhone Case Supplier Colorful iPhone 17 electroplated case so cool case
Product Tags
Tempered Glass Supplier, What 90 Minutes in the Factory Actually Tells You
October 22, 2026
Ines had one afternoon and three factory visits
The message came from Porto, in the tone people use when they've just realised they've been guessing. Ines buys for a Portuguese accessories distributor that sells into phone shops and two small chains, and she had finally booked a sourcing trip. Four days, three factories, one afternoon per factory, and a colleague's warning ringing in her ears: "everyone shows you the clean room and the certificates, nobody shows you the log".
She asked me the only question that mattered: in ninety minutes, what do I actually look at?
I've been on the other side of that visit maybe two hundred times, as the supplier being walked through his own floor. I've watched buyers spend fifty of their ninety minutes photographing a showroom and the remaining forty drinking coffee. I've also watched a German buyer with a clipboard find, in eleven minutes, something about our printing registration that we had been quietly tolerating for a year. She was right and we fixed it, and the fix cost less than the coffee.
So this is the version I'd give my own customer. Not a checklist of documents to request — you can get that by email. This is what you look at with your own eyes, in what order, and what number you should write down while you're standing there. It's written from the supplier's side, which means it includes the things we'd rather you didn't inspect.
The furnace log matters more than the showroom
Start with the furnace, not the showroom
Every tempered glass supplier in Shenzhen has a showroom. Roughly half of them have a furnace. Those two facts are related to your price in a way that nobody explains at the meeting.
The furnace is where glass stops being glass and becomes "tempered". Thermal tempering heats the sheet to somewhere around 650 to 700 degrees Celsius and then quenches it with air, fast enough that the surface cools and contracts before the core does. The result is a layer of compressive stress at the surface, typically in the hundreds of megapascals, which is what makes the sheet resist a hit that would shatter ordinary glass.
That process produces a log. Zones, temperatures, conveyor speed, quench pressure, cycle count, batch number, operator. Ask to see the last seven days of it. Three things matter more than the numbers themselves.
First, whether the log exists at all. A supplier who tempers in-house can print a log in thirty seconds. A supplier who buys finished sheets from someone else will produce a certificate with a supplier's name on it, and that is a different document with a different meaning. Neither is automatically bad — plenty of good trading houses exist — but you should know which one you're buying from, because it tells you where the quality argument stops being theirs.
Second, whether the log matches the cartons. Pick a batch number off a carton of finished goods on the rack, and ask for that batch's log. If the answer involves someone going to find a file and coming back with a different week, you have learned something worth the flight.
Third, whether the furnace has been calibrated this year. Six-monthly calibration is normal for the thermocouples. Ask for the certificate and look at the date, not the logo. An uncalibrated furnace doesn't produce obviously bad glass; it produces glass that passes on Tuesday and fails on Thursday, which is worse.
One more thing while you're standing there: count the sheets going in and the sheets coming out, for ten minutes. The gap between them is the scrap rate of the tempering step, and it belongs to a conversation about yield that we'll come back to.
The glass before your glass: where the sheet comes from
A screen protector begins as float glass, made by a handful of companies worldwide, and the sheet's provenance decides most of what happens later. Names you'll hear in this trade include Corning, AGC, Schott and the large Chinese float makers such as CSG, Xinyi and Kibing. The differences that matter to a buyer are not brand prestige. They are thickness tolerance, flatness, and the presence of tiny inclusions.
Thickness is the one you can measure yourself. A caliper on twenty sheets from three cartons, written down, tells you whether the "0.33 mm" on the quotation is a specification or a wish. A good sheet runs within about ±0.02 mm. When the spread is wider than that, two things follow: your drop performance becomes a lottery, and your lamination develops bubbles because the AB glue layer has to absorb the difference.
Ask to see the incoming inspection record for the last delivery of raw sheet. Not the COA from the mill — the record of what the factory did when the pallet arrived. If the answer is "we trust the supplier", then the thickness tolerance on your purchase order is decoration.
If the visit is long enough, ask to see a reject tray. Any working line has one. The contents tell you what this factory actually catches: chipped edges, bubbles, print misregistration, scratches. A tray full of nothing but edge chips is normal. An empty tray means the tray is a prop, and the rejects are going in the bin before you arrive.
The edge is where most of your returns are made
Corners and edges are where glass fails, and they are the cheapest place to cut a corner, literally. After cutting, the edge is ground and chamfered, usually to something in the range of 0.1 to 0.3 mm, and then polished. A properly finished edge removes the micro-cracks from the cutting wheel; a rushed one leaves them, and they are the starting point for the crack that appears three weeks after the customer fits the protector.
You can see this without equipment. Hold a sheet up to the light at an angle and look along the edge: it should be even, with a small, consistent bevel, and no white, crumbly flecks. Run a fingernail along it. A good edge feels like a smooth plastic ruler. A bad one feels like it catches, because it does.
Then count the machines and the people. CNC grinding is a bottleneck in every plant I've been in, and the ratio of grinders to laminating stations is one of the most honest numbers in the building. If a factory can laminate a hundred thousand pieces a month and grind thirty thousand, then seventy thousand of its "tempered" output has an edge that a machine never touched.
Ask what the edge breakage allowance is on the line. Three to eight percent on thin sheet is normal. A supplier who claims one percent at your price is either lying or buying finished sheets from someone who isn't.
The layer nobody inspects: AB glue
The adhesive is where a screen protector earns its white edges or its clean fit, and it's the component buyers inspect least, because it's invisible until it fails.
AB glue comes in thicknesses from about 0.1 mm to 0.25 mm, and lamination happens either under vacuum or through rollers, followed by an oven stage to drive out the trapped air. The number that matters is not the thickness on the spec sheet; it's the defect rate per thousand after lamination. Ask what the line's bubble reject rate is and watch whether the answer is a number or a story. Two to five percent is a working factory's reality on thin glue. Zero is a marketing position.
Then ask to see the inspection lamp. A proper inspection station has a light source behind a diffuser and a person who looks at every sheet, or a sample of every batch, for bubbles, dust, and scratches in the adhesive. If the plant has no dedicated lamp and no record sheet, the "100% inspection" claim in the brochure refers to a different factory.
One question worth asking, because the answer is usually honest: which glue brand do you use, and can I see the delivery note? AB glue is bought in rolls with lot numbers, and a factory that can show you the lot can also tell you which of your cartons was made with it. That traceability is worth more than a lower price, because it's the difference between a complaint you can investigate and a complaint you can only apologise for.
Tempered glass wholesale: one description, several constructions
9H is a coating, not a strength
Every quotation in this trade says 9H, and almost every buyer treats it as a hardness guarantee for the glass. It isn't. The pencil hardness scale measures how well a surface resists a scratch from a graphite pencil of a given grade. It says something about the coating on top of the glass. It says nothing about whether the sheet will survive a drop onto a tiled floor.
The number that speaks to break resistance is the compressive stress in the glass, which comes from the tempering or chemical strengthening step, and the test that speaks to it in practice is a ball drop. Our standard on the line is a 64 gram steel ball from one metre onto a mounted sample, five pieces per batch, with the result written down. It is not a perfect test — nothing in a factory is — but a supplier who can show you a book of daily ball-drop results is a supplier who tests.
Chemical strengthening, incidentally, is not the same as thermal tempering. It submerges the glass in a molten potassium salt bath at around 400 to 420 degrees and swaps smaller sodium ions in the surface for larger potassium ones, which puts the surface in compression. It suits thin glass better than an air quench does. If a supplier says "tempered" and shows you a salt bath, that's not a lie in the trade's loose vocabulary, but you should know which process is protecting your customer's screen, because the failure modes differ.
Ask both questions in the same breath: which process, and which test proves it. The second question separates the sales office from the floor.
The black border tells you about their printing
Almost every protector has a printed frame, and the print is a small manufacturing discipline that reveals a lot. Registration — how accurately the black border sits relative to the glass edge — is normally held to about a tenth of a millimetre on a decent line. When it drifts, you get a border that covers a sliver of the visible screen on one side and shows a hairline gap on the other.
Ask to see the registration sample: a sheet printed with a crosshair or a rule, checked under magnification, kept per shift. If the plant runs three passes of black to reach opacity, ask how many. One pass looks black on the shelf and grey on the phone. Two is standard for mid-range. Three or four is what a buyer paying for a premium line should be told about.
Inks matter for compliance too, though that's a subject for another piece. The short version for a factory visit: ask which ink system they use and whether they have a current test report for it. Any supplier who prints for the European market should be able to answer without leaving the room.
Three tests you can run in their own QA room
You don't need a laboratory to check a supplier's honesty. You need their QA room, their own equipment, and thirty minutes.
The ball drop. Ask them to run it while you watch, on a sample you pick from a carton you also pick. Watch where the ball lands and whether the sheet is supported the way the spec says. A test that is run differently for you than for the daily log is a test you've just invalidated.
The bend. A four-point jig measures how much force the sheet takes before it fails, and the number should be in the hundreds of megapascals for a properly strengthened 0.33 mm sheet. You're not auditing the absolute figure; you're auditing whether anyone in the building knows it.
The abrasion and the tape. A rubber eraser rubbed back and forth a hundred times on the surface tells you something about the coating's durability, and a piece of tape pressed on and pulled off tells you whether the oleophobic layer is bonded or just present. Cheap test, unpleasant results, useful conversation.
Then the one that no one offers: a temperature cycle. Take five samples, put them in a fridge for two hours and then in a warm room, and look at the adhesive edge afterwards. Cold-climate buyers should care about this more than they do, because a protector that lifts at −5 °C in a Finnish January is a return in February, and the glue that does it looks perfect in Shenzhen in October.
Yield explains the price more than the quotation does
Here's the part of a factory visit that most buyers skip, and it's the one that pays for the trip: ask for the yield, by step.
Cutting, grinding, tempering, lamination, printing, final inspection. Each step has a scrap rate. On thin sheet, grinding and lamination are usually the two biggest. If the numbers add up to a total yield in the high eighties, the factory is competent. If the claimed yield is 99 percent across all six steps, one of two things is true: the numbers are decorative, or the factory is buying finished goods and calling itself a manufacturer.
Why you should care: every point of scrap is a cost that has to land somewhere, and it lands in your unit price. A supplier with a 12 percent scrap rate and a supplier with a 4 percent scrap rate cannot both be quoting the same number and both be healthy. One of them is buying thinner sheet, cheaper glue, or a shorter temper — and you'll find out in the returns, eighteen months later, at your expense.
Three quotes, the same twenty thousand pieces
Numbers make the argument better than adjectives, so here is one from a real comparison we lost and then won back. Full-cover 0.33 mm protector, black frame, twenty thousand pieces, same model, three quotes: 0.42, 0.55 and 0.68 euros.
The 0.42 quote is not theft and the 0.68 quote is not greed. They are three different constructions wearing the same description. Break the 0.42 down and it usually looks like this: sheet at the thin end of the tolerance band and bought on price rather than flatness, glue at 0.10 mm, two print passes, edge cut and lightly touched rather than properly chamfered, one poly bag and a plain carton. The 0.68 quote carries 0.15 mm glue, a polished chamfer, four print passes, individual foam sleeving, and a scrap rate the factory actually knows.
The number that decides which one is cheaper is not on any of the three quotations. It's the return rate, and it's not visible for twelve weeks.
Do the arithmetic with your own numbers, but here's the shape of it. Take a 3 percent return rate on the 0.42 tempered glass unit. Returns don't only cost you the unit; they cost the unit, the outbound shipping, the handling, the customer service minute, and the review. In a small distribution business that lands somewhere between three and five times the unit price per return. At 20,000 pieces, 3 percent is 600 returns. Multiply by, say, 1.60 euro of all-in cost per return and you have 960 euros of damage on a product where the 13 cent saving was worth 2,600.
The 0.55 quote is the interesting one, because it's usually the honest middle: good sheet, 0.15 mm glue, three passes, chamfered edge, standard packing, and a factory that will tell you its scrap rate without blinking. Most of the programmes we supply sit there, and most of the returns conversations we never have come from there too.
Packing: the metre and a half nobody audits
Walk past the packing tables on your visit, because this is where a supplier's real cost discipline shows up, and where your breakage claims are born.
The elements are boring and specific. Every tempered glass protector goes into its own poly bag, or a foam sleeve, or between two foam sheets. Then a master carton, usually 500 or 1,000 pieces, with a divider or an inner box so the sheets don't slide. Then carton tape, corner protectors on export orders, and a pallet configuration that survives a forklift.
Ask three questions at those tables. How many pieces per carton, and is the carton's internal height matched to that count or to whatever box was in stock? Is there a corner protector on export cartons, and does it go on all four corners or two? And has anyone dropped a loaded carton from waist height this month, on purpose, and looked inside afterwards?
That last one matters more than it sounds. Glass doesn't usually break in a container because a container is rough. It breaks because a carton was under-filled, so the sheets had room to flex, or over-filled, so the top layer took the lid's weight, and then a pallet got stacked two high at a transshipment hub. The crack pattern in the claim photos will look like transit damage, and the cause will be a packing line that saved four cents.
The economics are trivial and the argument is not: corner protectors and inner dividers add somewhere around three to six cents per unit at these volumes. A container that arrives with an 8 percent breakage rate on 20,000 pieces costs you 1,600 units at your landed cost, plus the claim, plus the customer conversation. Nobody has ever won that trade.
Six weeks in a container, and why "cracked in transit" is usually packing
An export shipment of tempered glass protectors spends four to seven weeks in a steel box that crosses several climate zones, sits on a dock in the heat, and vibrates at frequencies nobody tests for. Two things happen to glass in that box: mechanical fatigue at the edges, and adhesive creep at the corners.
The mechanical part is why edge finish matters more than buyers expect. A polished chamfer tolerates vibration for weeks. A rough cut edge has micro-cracks, and vibration propagates them slowly, which is why a shipment can arrive with a handful of pieces cracked inside otherwise perfect packaging. If your claim photos show breaks that started at an edge and travelled inward, you're looking at the grinding line, not the freight forwarder.
The adhesive part is the reason a batch can arrive with corners lifting. AB glue softens in heat, and a container roof in July reaches temperatures that would surprise you. If the glue was laminated at the thin end of its range, or cured too fast, it shows up as lifting at the corners three weeks after arrival, and the customer blames the fit.
Both of these are auditable before you book freight: ask what the factory's transit claim rate is over the last year, in percent, and ask whether they air-freight launch orders rather than sea-freight them. A launch-week order that arrives by sea in week five is a launch missed; 20,000 pieces at twelve grams is 240 kilograms, and the air premium on that weight is a number you should see written down rather than guessed at.
The trial order that tests a supplier in a month
You don't need a hundred thousand pieces to find out who you're dealing with. A three-thousand-piece trial, run properly, will tell you most of it in four weeks.
Order three models and two colours, so the line has to change over. Ask for the batch numbers in advance, and for the glue lot with the shipment. On arrival, take twenty pieces from three different cartons and measure thickness with your own caliper, write the numbers down, and compare the spread against the tolerance you agreed.
Then fit ten of them yourself, on a real phone, in front of a window. Look for the border alignment, the lifting at the corners after a day, the touch response at the edges. Ten minutes with a window and a phone finds more than a page of inspection data.
Then break three on purpose. A protector that cracks from a waist-height drop onto tile is normal. One that cracks from a table-height tap is a sheet that was never properly strengthened, and no certificate will save that conversation.
And when something is wrong — because in a trial order something usually is — watch how the supplier responds. A supplier who asks for photographs, the batch number, and then sends a corrective action with a date is a supplier you can build a programme with. A supplier who offers a discount on the next order instead is telling you what their quality system is.
Three shapes of "supplier", and only one of them is a factory
The keyword in this trade is loose. A tempered glass supplier can be any of three things, and your contract, your audit and your risk all change depending on which one you've got.
The furnace owner. Glass in, tempered glass out, all under one roof, with the logs and the scrap trays to prove it. Highest control, highest minimums, and the least flexible on small custom programmes.
The laminator and printer. Buys tempered sheet from a furnace, adds glue, print, packaging and branding. This is the most common shape in Shenzhen and it's where most private-label programmes actually live. Perfectly legitimate, and the audit questions change: you're now auditing their incoming inspection of someone else's glass, not their furnace.
The trader. No floor, no furnace, no glue line; a good relationship, a sample library, and a list of factories. Sometimes the most useful partner for a small buyer with an awkward mix of models, because they'll consolidate. But the moment a quality problem needs a root cause, the trader has to go and ask somebody, and you are two steps away from the answer.
None of these is a moral failing. The failure is not knowing which one you're dealing with while telling your own customers that you've audited a factory.
The questions that make a sales manager uncomfortable
The visit has a rhythm, and the useful information comes after the comfortable part. Once the showroom tour is done, try these four in a row and watch the face rather than listening to the answer.
Which batch on that rack was made last Friday, and can I see its glue lot and its ball-drop sheet? What is your scrap rate at grinding, and who signs it off? Who supplies your AB glue, and what happens when a roll is out of spec? If I order the same model in three months, what stops the black border from moving a tenth of a millimetre?
Every one of them is answerable by a factory that owns its process. The answers you should be suspicious of are the smooth ones: "no problem", "100 percent", "we never have that issue". A real factory manager has a story about the last time that issue happened, and it usually starts with a supplier's name and ends with a change they made.
I'd also say this from our side of the table: a buyer who asks these questions gets a different level of service afterwards. Not because we like being interrogated, but because a customer who understands the process stops asking for the impossible at the same time as asking for the cheapest. That combination is what ruins programmes.
What we changed after being audited
The German buyer with the clipboard found two things. Our print registration was documented per shift but not per batch, so a complaint about a drifting border could not be tied to a run. And our ball-drop logs were kept in a notebook on the QA desk, which meant they existed but couldn't be produced for a customer six months later.
Both are now in the system: registration sample photographed and filed per batch, ball-drop results entered against the batch number rather than the date, and a folder per customer order holding the glass COA, the glue lot, the print registration photo, and the inspection sample photographs. It's dull, it takes twenty minutes per order, and it has ended three arguments in the last year before they became claims.
We also stopped quoting one number for "tempered glass" as if it were a single product. The line now quotes by construction: sheet thickness and source, glue thickness, print passes, edge finish, packaging. It makes our quotes longer and occasionally loses us a comparison against a one-line price. It also means the buyer can see exactly where the two cents went when they ask for a cheaper version, instead of discovering it in the returns.
Ask a screen protector wholesale supplier for the batch, not the brochure
Documents are a floor, not a roof
Everything you can request by email — the certificate of analysis, the 9H pencil report, the RoHS and REACH declarations for the inks, the ISO certificate on the wall — is a floor. It proves a sample existed and passed something at some point. It doesn't prove what was on the line on Tuesday.
Two specific holes are worth knowing about, because both are common and neither is fraud in the strict sense.
The first is sample identity. A test report names a sample description, not a production batch. "Tempered glass screen protector, 0.33 mm, clear" covers a dozen constructions, from a properly strengthened sheet to a thinned one that would fail the same test. Ask for the batch number to be written on the report if the product is going into a regulated channel, and check that the batch number format matches the one on your cartons.
The second is scope. A certificate for the glass says nothing about the glue, the print, the packaging or the oleophobic coating. Each of those has its own failure modes and, in Europe, its own paperwork. A supplier whose file is one PDF is a supplier whose file is thin.
None of this means the documents don't matter. It means the visit and the documents answer different questions: the file tells you whether they can do it, the floor tells you whether they are doing it this week. Buyers who only have the file are buying the supplier's optimism.
What we send a buyer before they come
Since a visit is expensive for both sides, we started sending a one-page brief a week before, listing exactly what a buyer will be shown and where the limits are. It began as a courtesy and turned out to be the most effective sales document we have, because it tells a serious buyer that we know what we can't show.
The six items are: the furnace logs for the last seven days, with the thermocouple calibration certificate; the incoming sheet inspection record for the last three deliveries, including the thickness measurements; the lamination line's bubble reject rate per thousand for the last month; the print registration sample per shift; the QA book with ball-drop and bend results against batch numbers; and the yield report by step, with the numbers that are ugly in it.
The brief also says what we don't have. We don't run a chemical strengthening bath, so anything below 0.33 mm in our range is thermally tempered sheet bought from a named mill, and the report will show the mill's name rather than ours. We don't print more than four passes on a frame because the fifth stops adding opacity and starts adding rejects. And our grinding line, not our laminating line, is the constraint on peak weeks, which is why a launch order booked in August ships in the order it was confirmed rather than the order it was promised.
A supplier who tells you the last of those before you ask is a supplier who has been audited enough times to stop pretending. That is the state you want your tempered glass supplier to be in.
What to do with the ninety minutes
If I had to compress the whole visit into an order of operations, it would be this. Furnace and its log first, because everything else is downstream of whether they actually temper. Incoming sheet and thickness records second, because flatness and tolerance decide the rest. The grinding line third, counted in machines and people. The inspection lamp and the bubble reject rate fourth. Printing registration sample fifth. Then the QA room, where you ask them to break something while you watch.
Write five numbers on the back of a business card before you leave: thickness spread, grinders per laminating station, bubble reject rate, total yield, and the date of the furnace calibration. Two suppliers visited the same day with those five numbers on paper will tell you more than a week of email.
And take the reject tray photograph. Not for the supplier — for you, in eighteen months, when a batch arrives that looks like the ones in it.
About We Accessory
We Accessory has supplied screen protectors and phone cases wholesale out of Shenzhen since 2012: tempered glass in 0.33 mm and 0.5 mm, full-cover and privacy constructions, 3D curved edges, matte and anti-blue-light finishes, plus the AB glue and print work that goes into a private-label programme. We run our own lamination and printing, and we buy tempered sheet from named mills, which means we can show you both the incoming inspection and the batch that came from it.
If you're preparing a factory visit, or you've just come back from one with a card full of numbers and no idea which of them matter, send them over. We'll tell you what's normal, what isn't, and which of your three candidates we'd put a first order with — including when the answer isn't us.
We Accessory
2F, Block A2, Nanchang Industrial Area, Xixiang Town, Bao'an District, Shenzhen, China
Tel: +86-755-36818832 · WhatsApp: +86-15919800304
Email: [email protected] · weaccessory.com
A tempered glass supplier is not audited by the folder of certificates handed over at the door. They're audited by what's on the floor at eleven in the morning, on a day you didn't choose, by a buyer who knows which five numbers to write down.
Share:


Why Choose We Accessory
12+
Years Experience
2000+
Product SKUs
50+
Countries Served
OEM
& ODM Service
2-4
Day Delivery
Professional Phone Accessories Wholesale Supplier
We Accessory is a trusted phone accessories wholesale supplier since 2012. We specialize in phone case, tempered glass screen protector, USB cable, charger and more mobile accessories wholesale, serving customers in 50+ countries worldwide.
Frequently Asked Questions
Where is We Accessory located?
We are located in Shenzhen
What products do you offer?
We offer phone cases, screen protectors, USB cables, chargers and more mobile accessories for all major brands.
Do you offer OEM/ODM services?
Yes, full OEM and ODM customization with your logo, packaging and designs.
What is your shipping time?
In-stock items ship in 2-4 business days via DHL/UPS/FedEx. Custom orders 5-7 days production plus shipping.
We Accessory (WeAccessory.com)
Address:2F, Block A2, Nanchang Industrial area, Xixiang Town,Bao'an District, Shenzhen
Tel: +86-755-36818832
Mobile/Whatsapp: +86-15919800304
Email: [email protected]
Microsoft Teams: william.shaw186
Product Tags
Contact us Now!
Please send us your Email address if you'd like some products


Copyright © 2012-2026 Shenzhen Western Electronic Co., Ltd All Rights Reserved. Sitemap | Best Phone Case Wholesale, Tempered Glass Screen Protector, USB Charger, Cable, other Mobile Accessories Wholesale